7 Best Defect Marking Systems for Buyers?

A Defect Marking System helps teams identify rejected parts before they move deeper into production. The right setup can make defects easier to see, sort, and trace. The wrong one may add delays or create marks that operators cannot read. It sounds simple. In practice, material, line speed, and inspection methods all affect the choice.

This guide reviews seven options buyers may encounter, from ink-based marking to laser and automated systems. Each approach has trade-offs. A mark that stands out on a metal component may not suit plastic, coated surfaces, or delicate products. Buyers should compare marking quality, cycle time, integration needs, maintenance, and the cost of consumables. Ask suppliers to test representative parts, not just polished samples. Check whether marks remain legible after handling and whether operators can verify them under normal factory lighting.

Reliable selection also depends on the production environment. A compact workstation may fit a low-volume cell, while a high-speed line may need automated detection and marking in one process. Consider data capture and traceability, too, especially when defects must be linked to batches or inspection records. No system is best for every factory. Some claims sound convincing until real parts are tested. The comparisons ahead are intended to help buyers ask sharper questions, assess practical limits, and shortlist equipment that fits their workflow. The final decision should still follow hands-on trials and a clear review of operating costs.
7 Best Defect Marking Systems for Buyers?

What Defect Marking Systems Do and How They Work

What Defect Marking Systems Do and How They Work

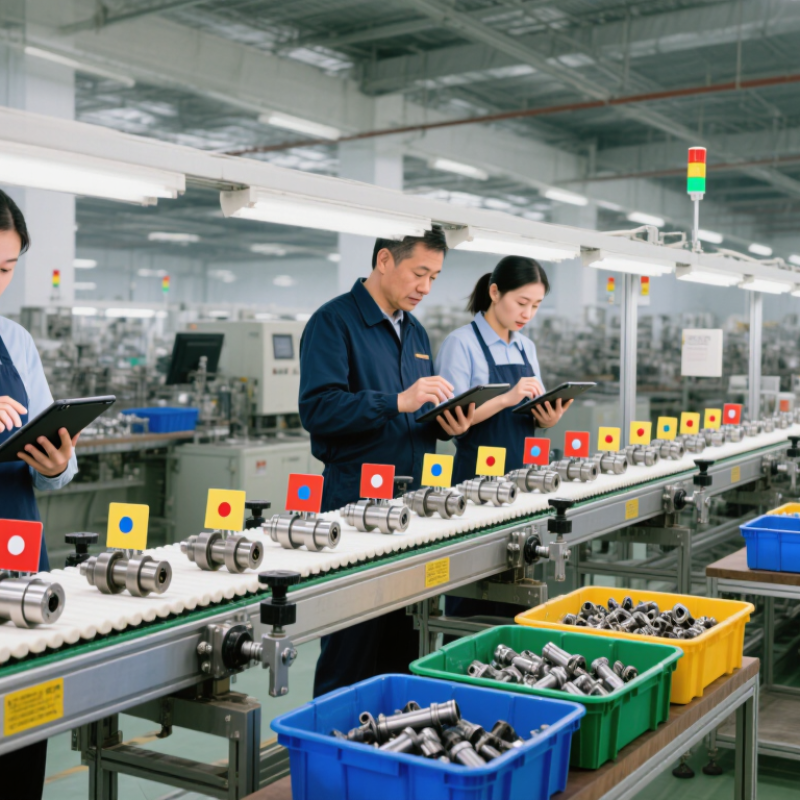
Defect marking systems locate product flaws and make them visible for sorting or repair. A camera or sensor scans each item as it moves along a conveyor or production line. Image software checks for issues such as scratches, discoloration, gaps, or incorrect dimensions. An encoder tracks the item’s position; when a defect is confirmed, a controller triggers an inkjet mark, label, or reject mechanism at the right spot. The mark helps operators find the fault without stopping the entire line.

Deloitte and MAPI’s 2023 Smart Manufacturing survey found that 86% of manufacturing executives viewed smart factory solutions as a likely competitiveness driver within five years. The International Federation of Robotics reported 553,052 industrial robot installations worldwide in 2022, reflecting broader growth in factory automation.

Performance depends on more than the camera. Lighting, surface glare, line speed, and mark contrast can all affect results. A system should record defect type and location, so teams can check patterns and trace recurring problems. Still, no setup catches everything. A glossy surface can fool a camera.

Tips: Test with real products and known defects, not just sample images. Check marks under normal factory lighting, and review missed detections during routine quality checks. Adjust thresholds carefully; overly sensitive settings can create false alarms.

Key Criteria for Evaluating Defect Marking Systems

A useful evaluation starts with marking accuracy. Check whether the system places a clear, consistent mark at the defect location, even when products shift slightly on the conveyor. Ask how it handles different materials, surface finishes, and line speeds. A mark that looks sharp on a clean sample may blur on damp or textured packaging. Small details matter.

Compare marking methods against the production environment. Consider the mark’s visibility, drying or curing time, and resistance to handling. Then review integration: Can the system receive defect signals from existing inspection equipment, and can operators adjust settings without slowing the line? Test it live. Use representative products and include normal speed changes, not just a steady demonstration.

Reliability involves more than uptime claims. Ask about routine cleaning, consumable use, changeover time, and access to service support. Track missed marks and false marks during a trial, then compare results across shifts. One limitation: short trials can overlook gradual nozzle buildup or changing product conditions. Buyers may also give too much weight to purchase price. A practical assessment should record operating costs and the time required to verify marked items.

Seven Defect Marking System Types Compared

Defect marking systems differ in visibility, permanence, and line speed. Inkjet printers apply small codes or dots to moving products, making them useful on fast conveyor lines. They need suitable ink and surface contrast. Laser marking creates durable marks without ink, but heat-sensitive materials may discolor. Test on a sample first.

Spray systems cover broad areas quickly, which helps inspectors flag large sheets or castings. Overspray can be a nuisance. Chalk marking is inexpensive and easy to remove, though dust and handling can erase it. Labels or tags preserve details such as defect codes and inspection dates, but adhesive may fail on oily or rough surfaces. Not always.

Mechanical punches make permanent marks on robust parts, yet they can deform thin stock. Robotic marking units move between positions and can apply different marks, but setup and programming take time. In practice, buyers should compare the mark against the next production step: will it survive washing, remain readable under shop lighting, or interfere with finishing? A neat mark is not automatically a useful one. Trials with actual materials often expose awkward issues, and selection can feel less tidy than a comparison chart suggests.

Matching Marking Methods to Materials and Production Lines

Choosing a defect marking system starts with the material, not the catalogue. Inkjet marks can suit fast-moving parts, but oily surfaces may cause smearing or poor adhesion. Laser marking creates durable marks on compatible materials, though heat-sensitive surfaces need careful testing. For large, rough components, paint pens or contact markers may be easier to control. There is no single best method.

The production line matters just as much. Check line speed, part spacing, surface temperature, and whether operators can reach the marking area safely. A mark must remain readable after washing, coating, or handling. Vision-triggered systems can help place marks consistently, but they depend on reliable part detection. Small setup errors can create misplaced marks across an entire shift.

Tips: Test samples under real line conditions, including dust, moisture, and normal handling. Compare contrast, drying time, and mark durability. Ask operators whether the mark is easy to spot from their usual position. A short trial may reveal awkward details that a specification sheet misses. Recheck the setup after material or line changes.

Installation, Integration, and Maintenance Considerations

Installation, Integration, and Maintenance Considerations

A defect marking system must fit the production line, not just the inspection station. Check available mounting space, conveyor speed, and the distance between detection and marking. A delay of only a few milliseconds can place a mark beside the defect instead of on it. Test with actual products, including dark surfaces, reflective packaging, and small flaws. Small details matter.

Integration needs equal care. Confirm how inspection signals reach the marking device and whether both systems use compatible timing and data formats. Run sample products at normal line speed, then check that each mark matches the correct defect record. Plan what happens if communication drops or the marker runs out of ink. A simple alarm can prevent hours of uncertain production, though it cannot fix every process gap.

Maintenance should be practical for the people on the floor. Keep access clear for cleaning sensors, replacing consumables, and checking alignment. Record routine checks and recurring faults; patterns may reveal vibration, dust, or changing product conditions. Keep spare parts nearby. One overlooked issue is that a system can pass commissioning and drift later as equipment wears. Schedule verification checks, and leave time for operators to report what feels awkward. Their feedback may expose a problem the setup checklist missed.

7 Best Defect Marking Systems for Buyers? - Installation, Integration, and Maintenance Considerations

System type How it marks Best suited for Installation considerations Integration considerations Maintenance and limitations
Continuous or drop-on-demand inkjet Applies small ink characters, dots, or codes without touching the product. Good fit: Fast-moving products, packaging, and surfaces that accept the selected ink. Mount the printhead at a stable distance and angle. Allow access for ink supply, cleaning, and adjustment; verify print performance on the actual surface. Can be triggered by a photoelectric sensor or encoder and controlled by a production-line PLC. Confirm line speed, product spacing, and mark position. Requires ink and, depending on the system, solvent or other fluids. Nozzles and printheads need routine cleaning; ink adhesion and drying vary by surface and environment.
Air-assisted paint or ink spray marker Sprays a visible spot, stripe, or short mark onto the product. Good fit: Large parts, lumber, metal stock, and applications where a prominent visual mark is needed. Provide a guarded mounting area, appropriate distance from the product, and suitable ventilation or overspray control. Check access to compressed air where required. Typically triggered by a sensor or PLC output. Coordinate the spray pulse with conveyor speed and product position; consider overspray near adjacent products. Uses replaceable or refillable marking fluid. Spray nozzles can clog and require cleaning; fluid choice must suit the material, drying time, and operating conditions.
Laser marking system Creates a visible mark by changing or removing material at the surface; it does not apply ink or a label. Good fit: Compatible products requiring a permanent mark, especially where consumable-free marking is valuable. Requires a controlled, guarded work area, suitable extraction for fumes or particulates, and protection appropriate to the laser class. Confirm the material can be marked as intended. Can be coordinated with sensors, encoders, vision inspection, and PLC or manufacturing software. Validate focus, product position, and marking time at production speed. No marking fluid is needed, but optics and extraction equipment need inspection and cleaning. Performance depends on material, surface finish, color, and process settings.
Automatic label applicator Applies a pressure-sensitive label carrying a defect status, routing instruction, or traceability code. Good fit: Products that need readable information, a scannable code, or a mark that can be removed later. Plan for label-roll loading, web routing, applicator clearance, and a surface suitable for label adhesion. Check application pressure and placement on the product. Often connects to a PLC, barcode or vision system, and production database to select label content. Confirm data rules and label timing before deployment. Requires labels and sometimes ribbon. Adhesion can be affected by dust, moisture, temperature, curvature, or surface energy; applicator pads and rollers need cleaning.
Dot-peen or impact marker Uses a pin to create a series of indented dots in the material. Good fit: Durable metal parts where a permanent, tactile mark is acceptable. Needs a rigid fixture and stable contact with the part. Check that the surface can tolerate impact and that vibration will not affect nearby equipment or the product. Can receive part data or marking commands from a controller. Positioning and cycle time should be tested against the line’s takt time and part variation. Inspect and replace worn pins as needed, and keep the marking head clean. The process is generally less suitable for delicate, thin, or soft products and very high-speed continuous lines.
Vision-guided marking station A camera locates a defect or feature, then signals a compatible marker or actuator to mark the selected position. Good fit: Products with variable orientation or defect locations that cannot be marked reliably at a fixed point. Provide stable lighting, camera mounting, a clear field of view, and guarding for the marking device. Capture representative samples to check detection and mark placement. Requires coordination among the camera, marker, PLC, conveyor encoder, and reject or sorting equipment. Define how the system handles missed detections and communication faults. Keep lenses and lighting clean and verify calibration periodically. Reflective, dirty, or changing surfaces can reduce detection reliability; maintain approved inspection recipes and backups.
Handheld marking tool An operator applies a marker, stamp, paint pen, or handheld label to the identified defect or product. Good fit: Low-volume production, rework areas, temporary inspection stations, and products that are difficult to present automatically. Provide an accessible work area, safe storage, and clear instructions for mark location and meaning. Consider operator reach and product handling. May be used independently or alongside a scanner or inspection record system. Standardize defect codes and recordkeeping if traceability is required. Low installation complexity, but consistency depends on training and adherence to procedures. Marking supplies need replenishment; manual marking can add labor and variation.
Go to Top